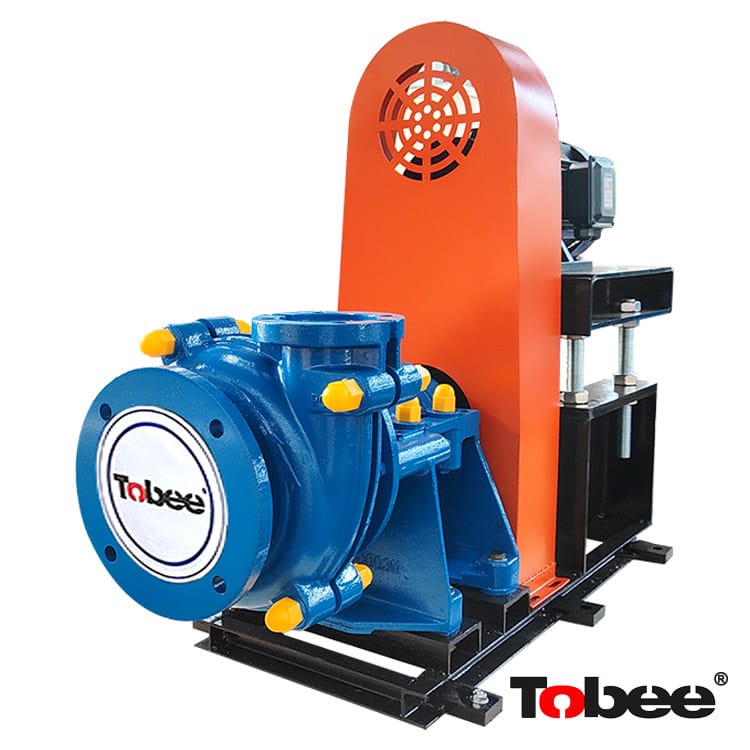
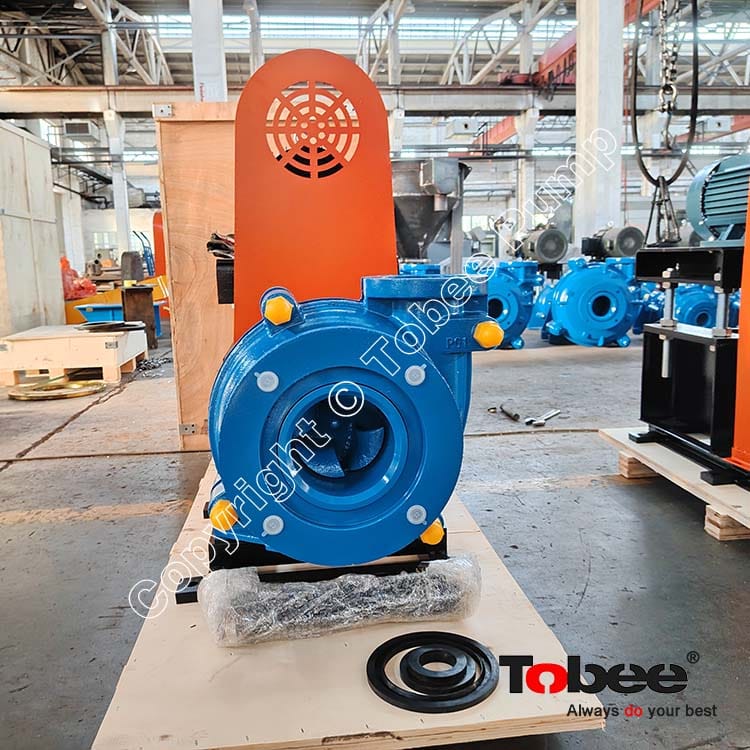
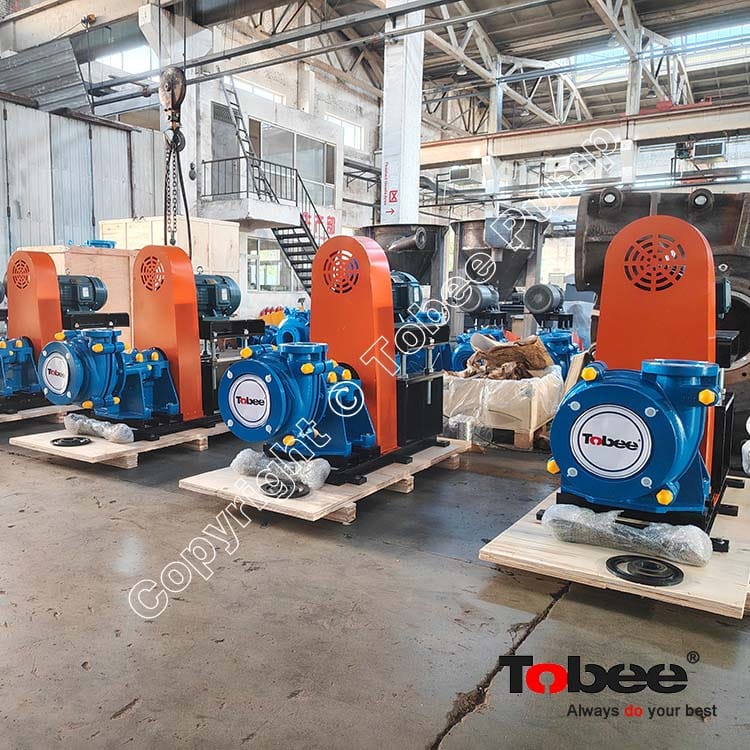
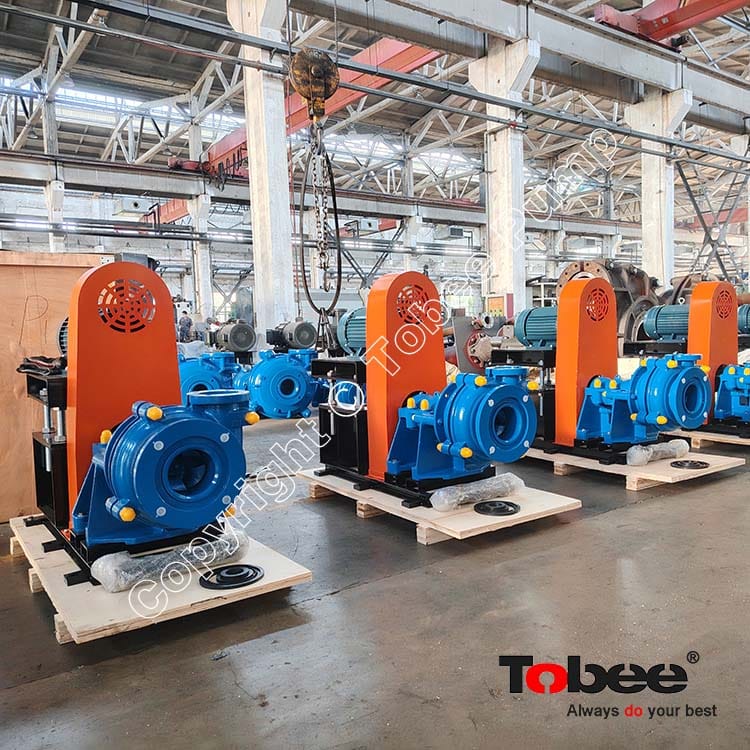
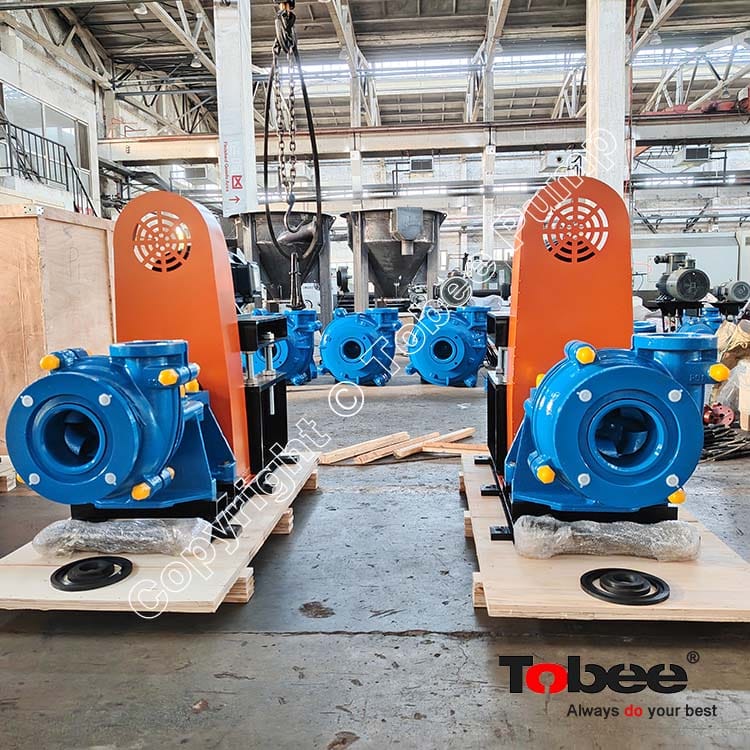
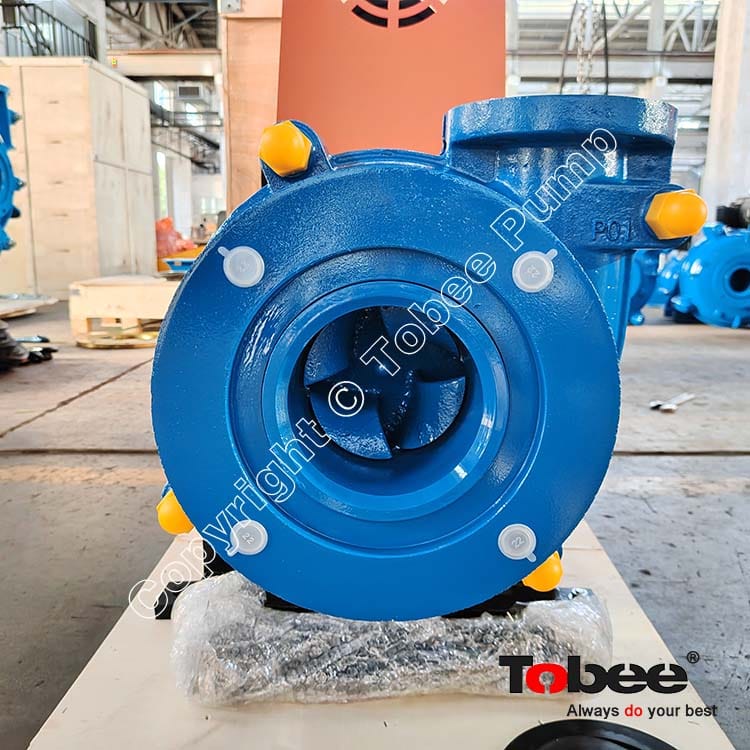
Tobee 2 AHF Horizontal Froth Slurry Pumps are designed for flotation circuits where space and flow requirements are constrained, AHF Pumps available in high chrome, rubber, polyurethane, and ceramic-lined configurations, and the pump handles solids concentrations up to 65% by volume and flows up to 200 m³/h.
Tobee® AHF Froth Slurry Pumps Design Features:
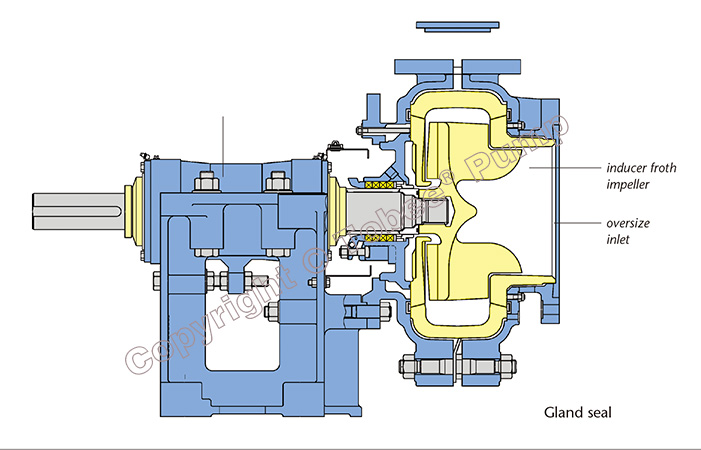
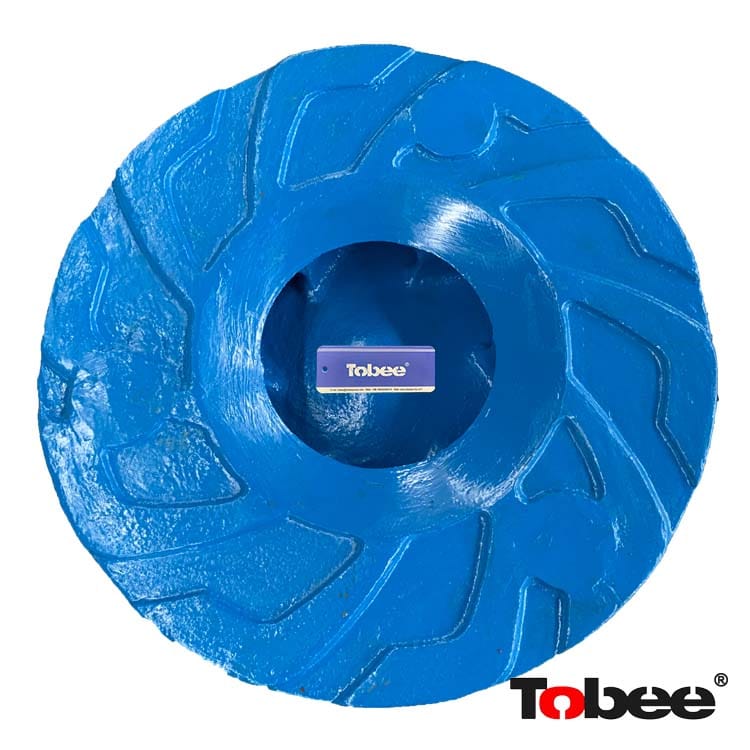
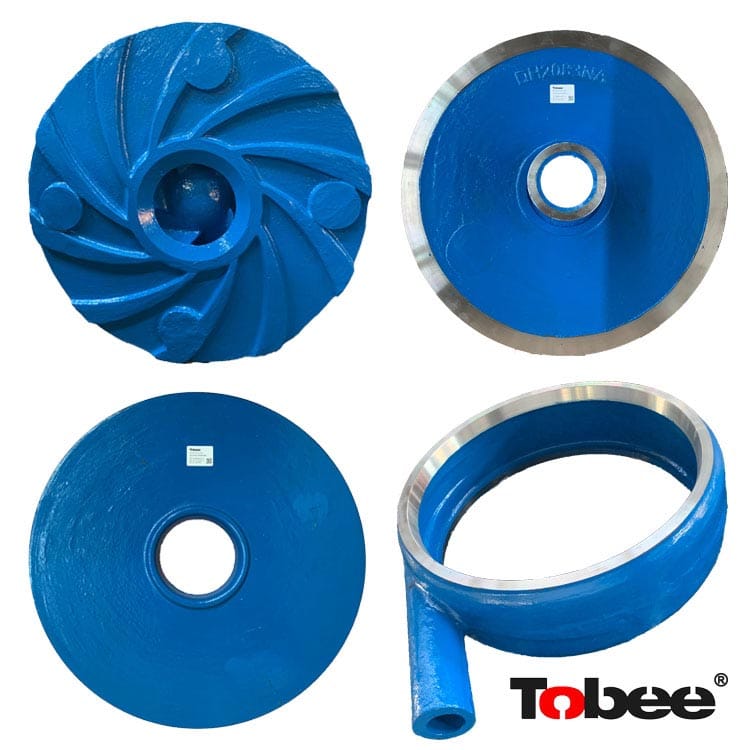
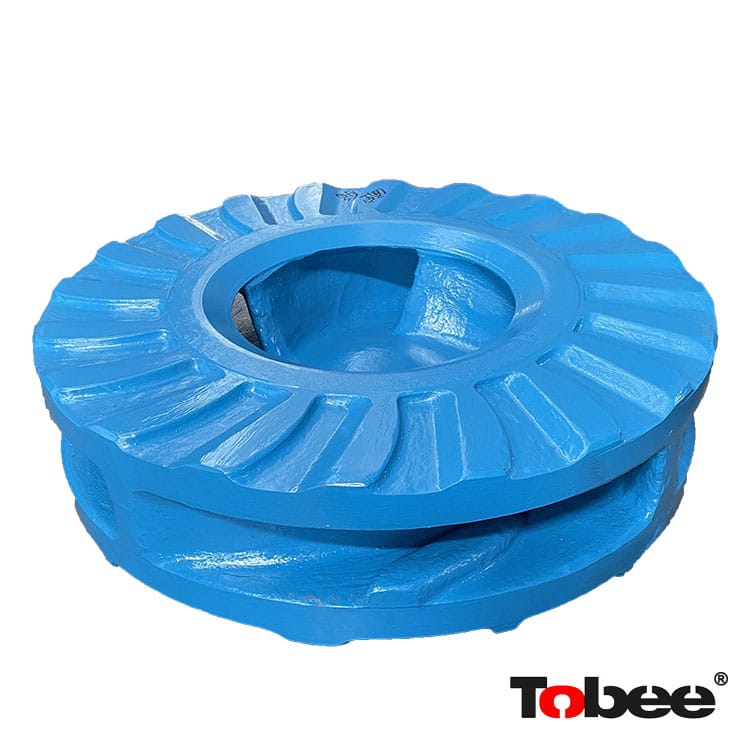
• Inducer Impeller: Features oversized inducer blades (scoops) on a semi-open impeller to promote froth entry, reduce air lock, and induce prerotation for efficient gas separation. This minimizes surging and improves stability at high Froth Volume Factors (FVF >2.0).
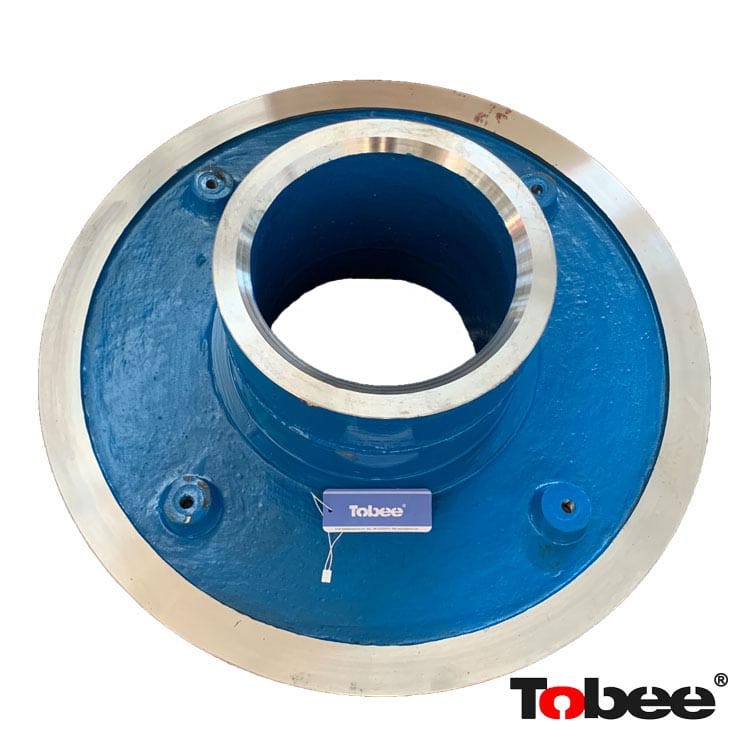
• Oversized Inlet and Throatbush: Large intake (3:1 inlet-to-discharge ratio) and enlarged high-efficiency throatbush maximize inlet area, lower NPSH requirements, and reduce internal velocities for extended wear life.
• Heavy-Duty Construction: Through-bolt frame design for easy maintenance and minimal downtime. Compatible with standard AH series mounting footprints for simple retrofits.
• Vented or Non-Vented Options: Optional Continuous Air Removal System (CARS) with venting holes and a gas collection chamber for superior handling of aerated slurries; non-vented version uses swirl-inducing impeller vanes.
• Wear-Resistant Components: Anti-abrasive liners and impellers (metal or elastomeric) with wide passages to handle viscous, non-Newtonian flows without clogging.
• Bearing Assembly: Grease-lubricated cartridge-style for quick replacement; low-vibration design reduces shaft failure risks.
These features ensure reliable operation in abrasive, high-air environments with efficiencies up to 80% under optimal conditions.
Tobee® AHF Froth Slurry Pumps Applications:
• Mining and Mineral Processing: Flotation cell discharge, concentrate transfer (e.g., copper, gold, zinc, molybdenum), and tailings handling in hard rock mines. Ideal for medium-froth conditions (FVF 1.5–2.0).
• Industrial Slurries: Coal washing, phosphoric acid processing, sand separation, and sugar cane refining.
• Other Uses: Pulp and paper mills, fuel gas desulfurization, wood processing, and any application involving viscous froths or aerated slurries with solids up to 65% concentration.
• Advantages in Use: Low power consumption, minimal surging, and reduced feed tank overflow; suited for low NPSH setups in flotation circuits.
Tobee® AHF Froth Pumps Structural Design:

 Added to subscribe successful !